
How to Choose the Right Flex Printed Circuit Board Supplier?
Choosing the right flex printed circuit board supplier can determine whether a product bends reliably or fails after repeated use. A prototype may look perfect on a clean workbench, yet crack near a copper transition after thousands of flexing cycles. Supplier selection must therefore examine more than price, lead time, or attractive sample boards.
Joe Fjelstad, a respected flexible-circuit technology expert, has observed, “Flex circuits are not simply rigid circuits with hinges.” This principle should guide every supplier evaluation. A capable partner understands polyimide materials, copper grain direction, bend radii, stiffeners, coverlay design, impedance control, and controlled manufacturing processes. Ask for evidence, not promises. Review process certifications, inspection records, material traceability, and previous projects with similar bending demands. A supplier experienced with medical, automotive, aerospace, or compact consumer devices may identify risks earlier.
Details matter.
Request cross-section samples and manufacturing capability data. Discuss dynamic bending, static folding, thermal cycling, solderability, and connector durability before approving the design. Factory visits, when practical, can reveal real conditions: organized material storage, clean inspection areas, calibrated equipment, and technicians who understand your drawings. However, no supplier is flawless. Early assumptions about bend life or delivery capacity may prove wrong. Build a qualification plan with measurable acceptance criteria, independent testing, and corrective-action procedures.
The strongest relationship is transparent and technical. Your chosen flex printed circuit board supplier should challenge weak design decisions respectfully, communicate limitations clearly, and improve alongside your engineering team. A reliable supplier does not merely manufacture the board. It helps protect the product’s performance in the field.
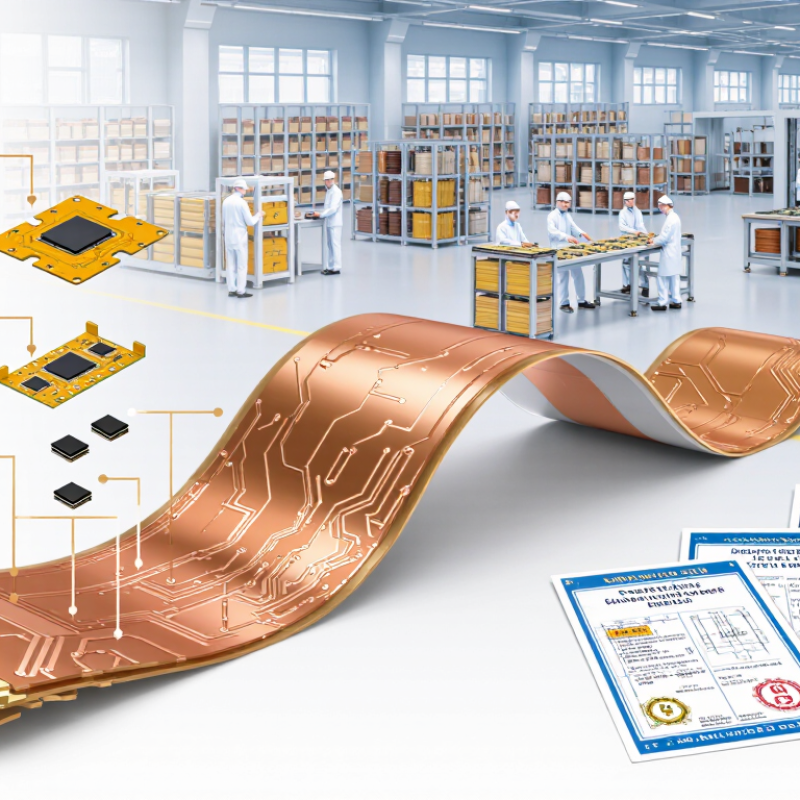
Define Your Flex PCB Requirements and Performance Targets
Before comparing suppliers, define what the flex PCB must survive. A wearable sensor may need thousands of bend cycles, while a camera module may bend only during assembly. State the bend type, minimum radius, bend zone, and expected cycle count. Specify board length, width, layer count, copper thickness, and acceptable thickness variation. Small details matter. A tight bend radius can expose weaknesses that a flat prototype hides.
Set electrical targets with measured conditions, not optimistic guesses. Record operating voltage, continuous current, peak current, impedance, signal speed, and allowable loss. Add temperature range, humidity exposure, vibration, and chemical contact where relevant. If the circuit carries heat, define thermal limits near connectors and stiffeners. Request stack-up drawings, material data, cross-section reports, and test evidence. Reliable suppliers should explain how they verify resistance, insulation, adhesion, and dimensional tolerances.
Your requirement sheet should also describe assembly realities. Include component weights, fold sequence, adhesive areas, connector clearances, and access for inspection. I have seen projects fail because the drawing showed a bend, but not the tool used to make it. Leave room for review. Early targets are often incomplete, and some may conflict. Ask the supplier to flag risks before fabrication, then revise the specification with recorded changes. That discussion reveals practical competence better than a polished sales promise.
How to Choose the Right Flex Printed Circuit Board Supplier?
Define Your Flex PCB Requirements and Performance Targets
| Requirement Area | Recommended Design Target | Supplier Acceptance Criteria | Why It Matters | Evidence to Request |
|---|---|---|---|---|
| Circuit Type | Single-sided, double-sided, or multilayer flex according to routing density and mechanical movement. | Demonstrated production experience with the required construction and comparable applications. | Construction affects flexibility, thickness, signal integrity, yield, and cost. | Process flow, representative samples, capability summary, and inspection records. |
| Layer Count | 2 to 6 conductive layers for typical compact flex designs; specify more only when routing or shielding requires it. | Stable registration and lamination capability across the required layer count. | Additional layers can improve routing but normally increase thickness and bending stiffness. | Cross-sections, layer-registration data, and first-article inspection results. |
| Finished Thickness | Approximately 0.10–0.30 mm in the bend area for many compact applications, excluding stiffeners where applicable. | Finished thickness tolerance defined on the drawing and measured at specified locations. | Thickness influences bend radius, packaging space, connector fit, and mechanical reliability. | Thickness map, gauge calibration records, and sample measurement report. |
| Copper Thickness | 18–35 µm finished copper for many signal layers; increase thickness when current or voltage-drop requirements demand it. | Controlled copper thickness with no unacceptable thinning at etched features or bend zones. | Copper thickness affects current capacity, resistance, flexibility, and etching resolution. | Microsection data, copper-thickness measurements, and electrical test results. |
| Minimum Line / Space | 100/100 µm for a practical baseline; 75/75 µm or finer requires process confirmation and adequate volume. | Verified imaging, etching, and inspection capability at the specified geometry. | Smaller features save space but may reduce manufacturing margin and yield. | Capability study, dimensional inspection data, and defect-rate information. |
| Bend Radius | At least 6 times the finished thickness for static bends; use a larger radius for repeated dynamic flexing unless validated by testing. | Supplier confirms bend-zone geometry, copper orientation, and cycle-life capability. | An overly tight radius can crack copper and shorten flexing life. | Bend-cycle test method, sample results, and design-for-flex review. |
| Dynamic Flex Life | Define the required cycles, bend angle, radius, speed, and electrical load; a preliminary target may be 10,000–100,000 cycles depending on use. | Passes the agreed cycle test without open circuits, intermittent faults, or unacceptable resistance change. | Cycle requirements vary significantly between a one-time installation bend and continuous motion. | Documented test plan, pre/post resistance data, and failure analysis procedure. |
| Impedance Control | Specify the required single-ended or differential impedance, commonly with a design tolerance of ±10% unless tighter control is necessary. | Controlled dielectric thickness, trace geometry, and test coupons for impedance verification. | Stable impedance supports signal quality in high-speed interfaces. | Impedance calculations, coupon reports, and time-domain reflectometry results. |
| Current-Carrying Capacity | Specify continuous and peak current, allowable temperature rise, conductor width, and copper thickness; do not rely on trace width alone. | Supplier validates the design against recognized conductor-heating guidance and the actual operating profile. | Flex circuits dissipate heat differently from rigid boards because of their thin construction. | Thermal calculations, temperature-rise testing, and conductor cross-section data. |
| Operating Environment | Define temperature, humidity, vibration, chemicals, and mechanical shock; a common initial range is −40°C to +85°C when applicable. | Materials, adhesives, coverlay, and finishes are rated for the complete environmental profile. | Environmental exposure can affect adhesion, insulation, corrosion resistance, and flex life. | Material datasheets, environmental test reports, and qualification samples. |
| Surface Finish | Select finish according to contact life, soldering process, storage period, and cost; define thickness and contact requirements. | Uniform finish coverage, controlled thickness, solderability, and compatibility with assembly processes. | The finish affects corrosion resistance, contact reliability, solderability, and shelf life. | Finish-thickness report, solderability data, and visual inspection criteria. |
| Stiffeners and Connectors | Define stiffener material, thickness, location, insertion area, bend keep-out zones, and connector mating requirements. | Accurate stiffener placement and dimensional control at all mating and assembly features. | Stiffeners provide support where the flex circuit must be inserted, mounted, or soldered. | Dimensional inspection report, connector-fit samples, and assembly trial results. |
| Reliability and Qualification | Establish thermal cycling, humidity, bend, vibration, soldering, and insulation-resistance tests based on the application risk. | Written qualification plan with pass/fail limits, sample size, traceability, and corrective-action process. | Qualification reveals failure mechanisms before production release. | Reliability reports, failure-analysis records, and lot traceability documentation. |
| Quality and Compliance | Require a documented quality system and compliance with the standards specified for the intended market and product category. | Current certificates, controlled documentation, inspection records, and change-notification procedures. | Consistent processes reduce variation, escapes, and supply-chain risk. | Quality certifications, audit results, control plan, and nonconformance statistics. |
| Prototype-to-Production Support | Define prototype quantity, production volume, target lead time, annual demand, and expected ramp schedule before supplier selection. | Clear quotation, design-for-manufacturing feedback, repeatable lead times, and capacity planning. | A supplier must support both early design learning and stable volume production. | Sample build schedule, capacity statement, yield trend, and engineering change process. |
Related Posts
-
2026 Best Flexible Printed Circuit Board Suppliers?
-
How to Choose the Right PCB Flex Supplier
-
What Is PCB Flex and What Types Are Available?
-
10 Essential Tips for Designing High-Quality PCB Flex Circuits
-
What Are the 7 Best PCB Types for Global Buyers?
-
Understanding the Essential Role of Printed PCBs in Modern Electronics